Challenge 01
Complex Assembly Operations
Multiple components, product variants, and manufacturing stages make production coordination challenging.
“Which variant is on SMT Line 2, and will WO-4410 finish today?”Production manager
Electrical & Electronics
From component assembly and testing to final inspection, DelphEon helps electrical and electronics manufacturers monitor production performance, manage execution activities, and maintain connected quality and manufacturing records.
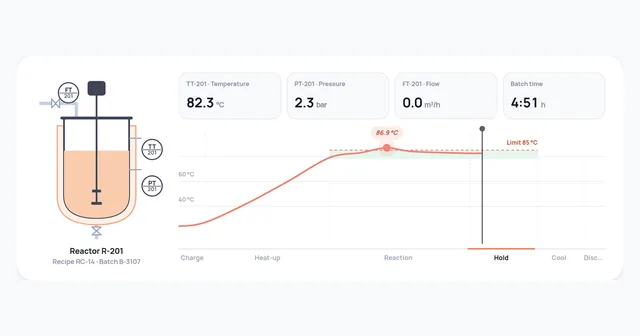
Scroll to watch:Shown here: Standing-loss test on an 80-litre water heater
Test bay 3 · WH-80 · SN 26-1142
Every step, reading and result in one test record.
Multiple components, product variants, and manufacturing stages make production coordination challenging.
“Which variant is on SMT Line 2, and will WO-4410 finish today?”Production manager
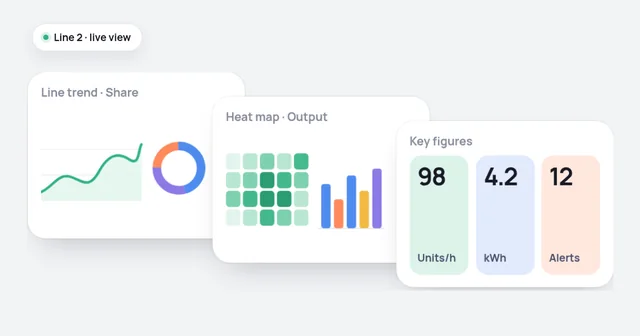
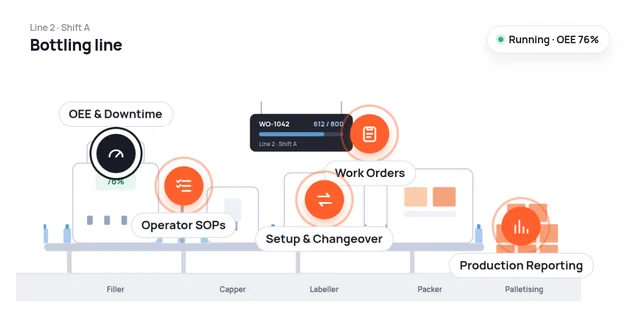
Monitor production progress, equipment performance, and actual output across assembly operations to identify delays and improve coordination.
On Line 2WO-4410 for CB-310 boards: 412 of 500 built, with SMT Line 2 running at 38 seconds per panel.
Key measuresProduction Output·Cycle Time·Work-Order Progress
Explore Shop Floor ExecutionDisconnected test results and inspection records make defect analysis and follow-up difficult.
“Why are boards failing the functional test on output voltage?”Quality engineer
Capture inspection results, testing information, and quality deviations to support structured reviews and faster investigation of production defects.
On Line 2FCT-1 failed 9 boards on low output voltage this shift, each logged with its serial number and test values.
Key measuresTest Results·Rejection Rate·Quality Deviations
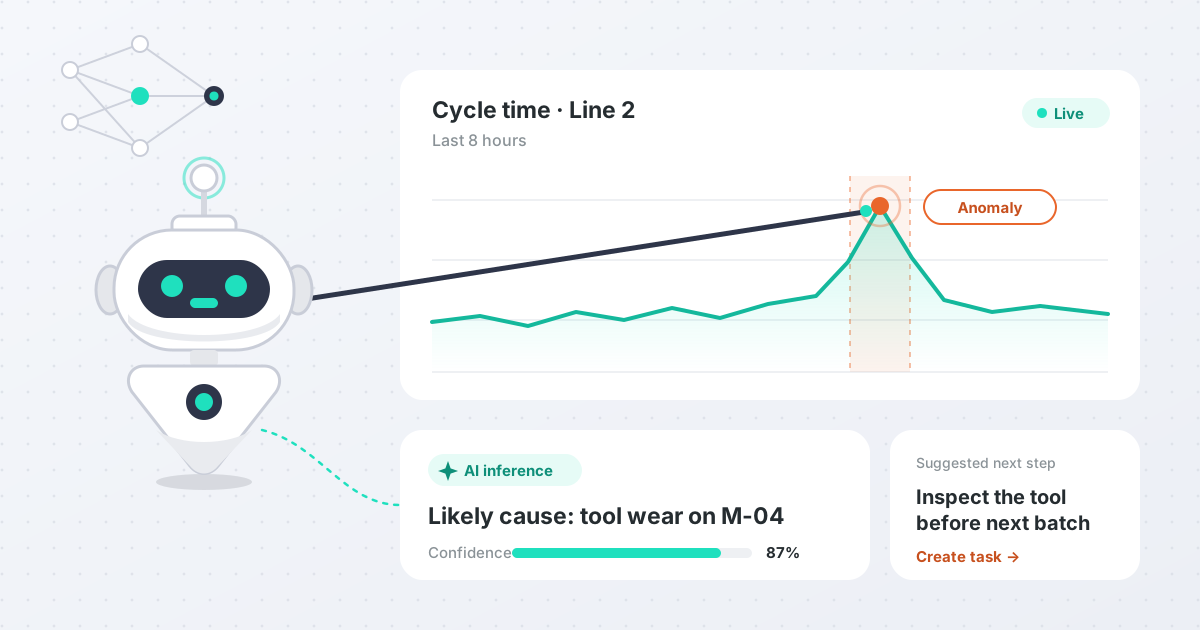
Explore Quality Management & TraceabilityEquipment stoppages, cycle-time variations, and bottlenecks affect output and delivery schedules.
“Why does the pick-and-place keep stopping on feeder errors?”Maintenance head
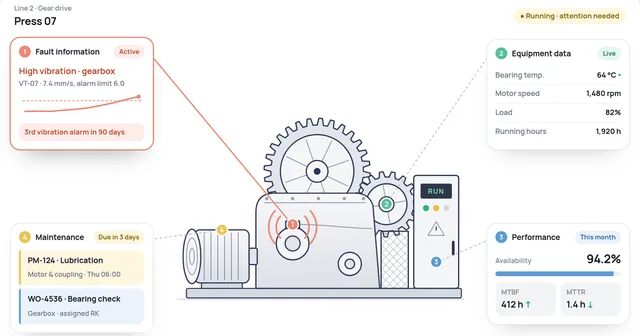
Track equipment utilization, stoppages, and recurring faults across assembly, testing, and other production operations.
On Line 2The pick-and-place stopped 7 times on feeder errors, 46 minutes in all, and line OEE fell to 74%.
Key measuresOEE·Downtime·Equipment Availability
Explore Asset MaintenanceTracking component lots, assembly records, and related quality information can require extensive manual effort.
“Which other boards were built with capacitor lot R-5531?”Quality head
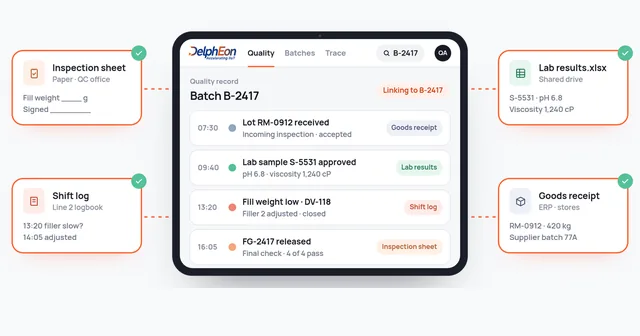
Associate available component, lot, and production information to support manufacturing history reviews and identification of potentially affected products.
On Line 2Start from board SN 24-0918 and find its capacitor reel lot R-5531, the stations it passed and its test results.
Key measuresLot History·Inspection Records·Traceability
Explore Quality Management & Traceability01 / 04
Stage by stage
One view from component stores to final inspection, built around the stages an electrical and electronics plant actually runs.
Reel lots issued against a paper kit list
Component lots and reels linked to the work order they were issued to.
Line stops noticed when someone reports them
Line status, cycle time, and feeder and nozzle stops for every SMT line.
AOI defects reviewed at the machine and cleared
Inspection results and defect counts linked to the board and station.
Variant progress tracked on a whiteboard
Work-order progress, variant mix and station output by shift.
Test logs kept on each tester’s PC
Functional and in-circuit test results linked to each serial number.
Serials matched to cartons by hand
Inspected and packed serials linked to shipment records.
One board, traced
A product may pass through multiple assembly and testing stages before reaching final inspection.
DelphEon helps bring available production activities, inspection records, and testing information together, making it easier to investigate issues and review manufacturing history.
C14Capacitor from reel lot R-5531, placed on SMT Line 2
SN 24-0918WO-4410 · Station 3 · Shift B
FailedFCT-1 · output voltage below limit
✓ DoneOther boards from lot R-5531 identified for review
Getting started
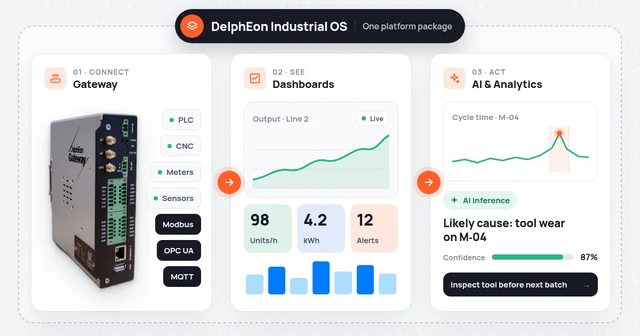
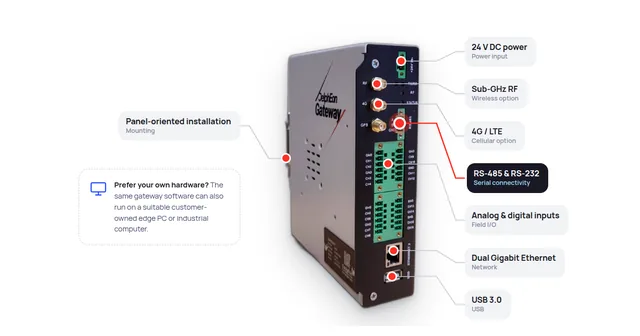
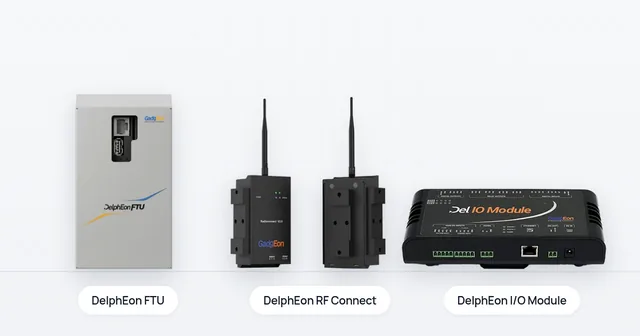
SMT lines, testers with a supported interface, PLCs and older machines connect through DelphEon Gateway using OPC UA, Modbus, S7 or MELSEC, or through I/O signals where there is no controller interface.
Begin with one line or product that includes testing and final inspection, and show a full trace from a packed serial back to its component lots.
Add lines, products and plants once the first line’s records are trusted. Your ERP keeps its existing responsibilities.
FAQ
DelphEon links assembly, test and inspection records to the identifiers your plant already uses, such as serial number, lot or work order. How serials and component lots are captured, for example by barcode scan or operator entry, is agreed at the start.
Test stations that expose results through a supported interface can be connected through DelphEon Gateway. Where they cannot, results can be recorded against the serial number at the station. Each tester is assessed during scoping.
No. DelphEon works alongside your existing ERP and quality systems. Which system owns orders, stock and quality records is agreed during scoping.
With one line or product that includes testing and final inspection. The aim is a complete, trusted record for that line before you expand.
Connect assembly activities, equipment performance, testing information, and traceability records to support more consistent electrical and electronics manufacturing operations.
Discuss Your Manufacturing Requirements